
 REALISING CAPITAL OUTCOMES
Manufactured capital
Manufactured capital
All the South African manufacturing sites have been declared as national key points during the year.
Manufacturing facility:
CLAYVILLE
PURPOSE
A state-of-the-art highly-automated high-volume liquids facility and a powders and effervescent plant.
BOOK VALUE
R749 million(2017: R692 million)
property, plant and equipment
CAPACITY PER ANNUM |
CAPACITY UTILISATION |
PROGRESS DURING THE YEAR |
|||
28 million 400 tonnes |
75% 70% |
All good manufacturing practice (GMP) upgrades to the general plant packing facility (Phase I) were completed during the year and all lines are up and running. A design and costing for Phase II has been prepared. The construction of the ophthalmic facility is on track for completion in the last quarter of calendar 2019. |
|||
12 million ℓ |
ACCREDITATIONSSouth Africa (SAHPRA), Ghana (FDB), Malawi (PMPB), Kenya (PPB), Zimbabwe (MCAZ), and Ethiopia (FMHACA). |
Manufacturing facility:
WADEVILLE
PURPOSE
A tablet and capsule facility which is focussed amongst others, on the manufacturing of anti-retroviral medicines, and a liquids, creams and ointments facility.
BOOK VALUE
R224 million(2017: R181 million)
property, plant and equipment
CAPACITY PER ANNUM |
CAPACITY UTILISATION |
PROGRESS DURING THE YEAR |
|||
6 million ℓ 500 tonnes |
80% 60% |
The second phase of the upgrade to the Liquids, Creams and Ointment facility was completed during the year and completion of the final phase is expected by early 2020 calendar year. |
|||
2 billion |
ACCREDITATIONSSouth Africa (SAHPRA), Ghana (FDB), Malawi (PMPB), Kenya (PPB), Zimbabwe (MCAZ), and Botswana (DRU). |
Manufacturing facility:
AEROTON
PURPOSE
The Critical Care facility produces intravenous fluids, blood collection bags, renal dialysis products and smallvolume parenterals.
BOOK VALUE
(2017: R367 million)
property, plant and equipment
CAPACITY PER ANNUM |
CAPACITY UTILISATION |
||||
33 million |
4 million |
100% |
|||
|
35 million |
1 million |
ACCREDITATIONSSouth Africa (SAHPRA), and Kenya (PPB) |
Manufacturing JV facility:
BANGALORE
PURPOSE
This facility produces tablets and capsules as a contract manufacturer for various pharmaceutical companies.
BOOK VALUE
R154 million(2017: R168 million)
property, plant and equipment
CAPACITY PER ANNUM |
ACCREDITATIONS |
PROGRESS DURING THE YEAR |
|||
3.5 billion CAPACITY UTILISATION90% |
UK (MHRA), Australia (TGA), South Africa (SAHPRA), France (ANSM), Tanzania (TFDA), Ghana (FDB), Namibia (NMRC), Kenya (PPB), Uganda (UNDA), Ethiopia (FMHACA), Zimbabwe (MCAZ), Malawi (PMPB), and Nigeria (NAFDAC). |
The manufacturing building (Unit 2) adjacent to the current factory, was acquired in July 2018. Construction will begin in the first quarter of the 2019 financial year and the entire capital expenditure of INR160 million will be funded from internal cash resources in the joint venture. |
DISTRIBUTION
“Services to meet your needs from your door to the country and beyond.”
This year has seen the rebranding of the Distribution Division, together with the acquired Virtual Logistics business, to AVL Healthcare. AVL has an extensive national footprint, is fully compliant with pharmaceutical standards and delivers over a million units per trading day through 13 sites to hospitals, wholesalers, the Department of Health, pharmacies, clinics, healthcare practices and retail outlets.
AVL is committed to provide exceptional service through the broad range of offerings that are tailored to meet specific customer needs.
DISTRIBUTION CENTRES AND/OR HUBS ARE IN THE FOLLOWING AREAS
- Midrand (2)
- Aeroton
- Clayville
- Cape Town
- Durban
- Bloemfontein
- Port Elizabeth
- Nelspruit
- Polokwane
- Kimberley
- East London
- Ladysmith
THE BROAD RANGE OF DISTRIBUTION SERVICES INCLUDE
Bulk
We have invested heavily in bulk warehouse storage, allowing us to meet customers’ bulk requirements every step of the way. Regardless of pallet quantity, we offer deliveries, inter-depot transfers and line haul service.
Fine
We deliver directly to healthcare customers, be they doctors, pharmacies, clinics, hospitals or wholesalers. Our state-of-the-art fine picking system allows us to better manage our warehouse throughput and provide a comprehensive logistics solution for our partners.
Retail
In the fast turnaround retail industry, the importance of efficient and reliable logistics cannot be over-emphasised. We offer fast, reliable delivery to all back-door retail outlets and distribution centres.
Cold chain
We offer validated fridge-to-fridge (in-vehicle) delivery capability at 2 – 8 degrees Celsius and are able to supply validated cold chain boxes. This ensures that temperature-sensitive deliveries are never compromised, no matter where they are along the supply chain.
Cold chain
We have invested heavily in bulk warehouse storage, allowing us to meet customers’ bulk requirements every step of the way. Regardless of pallet quantity, we offer deliveries, inter-depot transfers and line haul service.
Fixed fleet
We offer the supply and management of dedicated and validated healthcare specific fleet solutions. Our trucks are an extension of our warehouses, and offer a consistent and controlled environment at all times. Our fleet is validated and temperature controlled, our drivers are trained on standards operating procedure (SOP’s) and all trucks are tracked on a transport management system (TMS).
Inter-depot transfers
We offer compliant inter-depot transfers around the country.
Home patients
We offer delivery direct to patients for the Adcock Ingram Critical Care renal division.
Reverse logistics
We offer effective, professional management of customer returns.
Warehousing
Our warehousing solutions are designed to ensure a consistent storage environment for all pharmaceutical products.
Cross-border
Our footprint includes cross-border delivery. We offer direct loads and break-bulk loads to SADC countries.
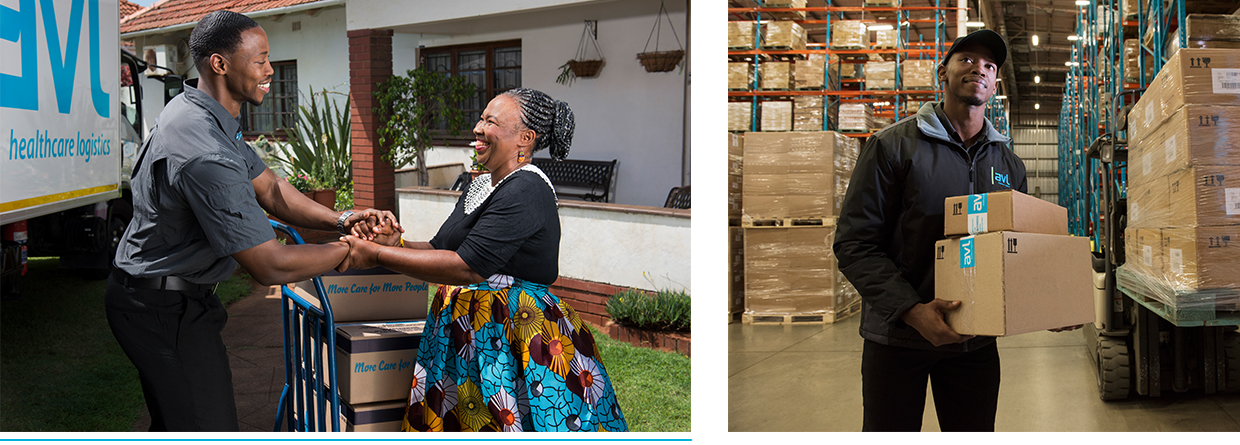
Making a home delivery to a renal patient.